A Practical Guide to Equipment Reliability, Condition Monitoring, Root Cause Analysis and Maintenance Optimization
Steel plants operate in one of the most demanding industrial environments.
High temperature, heavy loads, continuous operation, vibration, dust, scale, water, electrical stress, hydraulic pressure, mechanical shock and aggressive operating conditions continuously challenge plant equipment.
A single failure of a critical motor, gearbox, pump, bearing, hydraulic system, cooling-water pump, crane, rolling-mill component, furnace auxiliary system or electrical panel can interrupt an entire production sequence.
The cost of a breakdown is therefore much greater than the cost of the failed component.
It can include:
Production loss
Emergency maintenance
Spare-parts consumption
Overtime
Product-quality problems
Reheating or remelting losses
Delayed dispatch
Safety risks
Secondary equipment damage
Increased energy consumption
Loss of customer confidence
For this reason, modern steel plants need to move from a "repair after failure" philosophy toward a system based on:
Prevent → Detect → Diagnose → Plan → Repair → Verify → Improve
Predictive-maintenance research in the steel industry increasingly combines sensor data, condition monitoring and data-driven models. A Tata Steel case study, for example, investigated data-driven bearing-wear prediction using industrial production data and compared several machine-learning approaches.
The objective of this article is to explain how a steel plant can build a practical maintenance and reliability system that reduces unexpected breakdowns.
1. What Is a Breakdown?
A breakdown occurs when equipment can no longer perform its required function.
However, equipment failure should not be understood only as:
"The machine stopped."
A failure can occur in several forms.
Functional failure
The equipment cannot perform its required function.
Example:
A cooling-water pump is running but cannot deliver the required flow.
Partial failure
The equipment continues operating but its performance has degraded.
Example:
A hydraulic pump still operates but pressure has gradually fallen.
Incipient failure
The equipment is still operating, but measurable abnormality indicates developing damage.
Examples:
Increasing bearing vibration
Increasing bearing temperature
Increasing motor current
Gearbox oil contamination
Electrical hot spot
Hydraulic pressure fluctuation
This third category is extremely important.
Incipient failure is where predictive maintenance creates the greatest opportunity.
2. The Failure Development Process
Many equipment failures do not happen instantaneously.
A simplified failure-development process is:
Normal operation
↓
Small abnormality
↓
Degradation begins
↓
Condition changes
↓
Performance decreases
↓
Functional failure
↓
Breakdown
The interval between the first detectable abnormality and functional failure is often called the P-F interval in condition-based maintenance.
The P-F concept is fundamental to maintenance planning.
If a bearing starts developing a defect today but the machine will not fail for several weeks, maintenance has an opportunity to intervene.
The challenge is to detect the condition early enough.
3. Why Steel Plants Are Particularly Vulnerable
Steel plants combine several difficult operating conditions.
3.1 High temperature
Heat accelerates:
Lubricant degradation
Insulation ageing
Bearing deterioration
Seal failure
Hydraulic-oil degradation
Cable deterioration
Mechanical distortion
3.2 Dust and scale
Dust can enter:
Bearings
Motors
Gearboxes
Electrical panels
Hydraulic systems
Cooling systems
Scale can damage moving components and seals.
3.3 Heavy mechanical loads
Rolling mills, cranes, conveyors, charging systems and material-handling equipment experience substantial loads.
Shock loading can be particularly damaging.
3.4 Continuous operation
Equipment running continuously has fewer natural opportunities for inspection and maintenance.
3.5 Water
Steel plants use large quantities of water.
Water leakage or ingress can create:
Bearing damage
Lubricant contamination
Electrical faults
Corrosion
Hydraulic contamination
Foundation deterioration
3.6 Thermal cycling
Equipment may repeatedly experience heating and cooling.
This can contribute to:
Thermal fatigue
Cracking
Loosening
Expansion-related alignment problems
Refractory damage
Electrical connection problems
4. Maintenance Strategies Used in Steel Plants
A mature maintenance organization normally uses several maintenance approaches.
4.1 Breakdown Maintenance
Equipment is repaired after failure.
Advantages
Simple
Low planning requirement
Suitable for some non-critical equipment
Disadvantages
Unexpected downtime
Production losses
Emergency maintenance
Secondary damage
Safety risks
Higher repair costs
Breakdown maintenance should generally be limited to equipment where failure consequences are acceptable.
5. Preventive Maintenance
Preventive maintenance is performed before failure according to a defined schedule.
Examples:
Bearing lubrication
Gearbox oil replacement
Motor inspection
Filter replacement
Bolt tightening
Belt replacement
Coupling inspection
Hydraulic filter replacement
Electrical panel inspection
Schedules can be based on:
Calendar time
Running hours
Number of heats
Production cycles
Number of operating strokes
Tonnes processed
Equipment condition
Problem with purely time-based maintenance
If a bearing is replaced every 12 months simply because the calendar says so, the bearing may still have considerable useful life.
Alternatively, another bearing may fail before 12 months because of abnormal loading or lubrication problems.
Therefore:
Time-based maintenance alone is not sufficient for critical equipment.
6. Predictive Maintenance
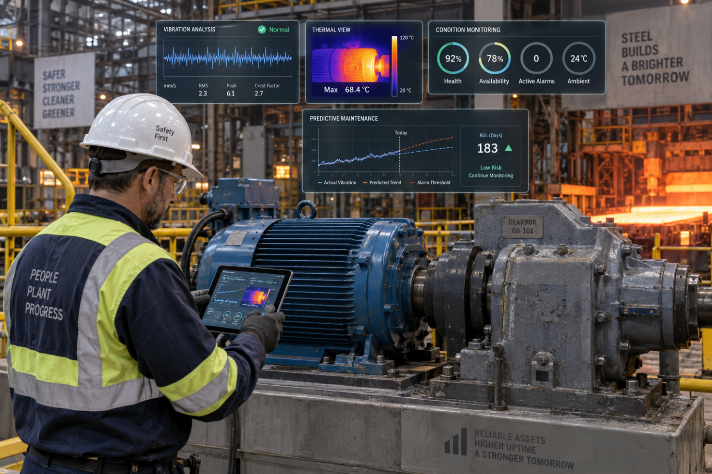
Predictive maintenance uses actual equipment-condition information to determine when intervention is required.
Common technologies include:
Vibration analysis
Infrared thermography
Oil analysis
Ultrasonic inspection
Motor current analysis
Temperature monitoring
Pressure monitoring
Flow monitoring
Electrical testing
Acoustic monitoring
Online sensor systems
The basic sequence is:
Measure → Trend → Analyze → Diagnose → Decide → Act
Predictive maintenance is particularly valuable for critical rotating equipment.
7. Condition-Based Maintenance
Condition-based maintenance uses equipment condition to determine maintenance requirements.
Instead of:
Replace bearing every 12 months.
The approach becomes:
Monitor bearing condition and replace it when evidence indicates unacceptable degradation.
This can reduce unnecessary maintenance while improving failure prevention.
8. Reliability-Centered Maintenance
Reliability-Centered Maintenance, or RCM, asks a more fundamental question:
What must the equipment do, how can it fail to perform that function, why does it fail, and what maintenance task can effectively manage that failure?
RCM has also been studied specifically in steel-melting-shop applications, where failure modes and effects are used to determine appropriate maintenance categories.
A practical RCM process is:
Function
↓
Functional failure
↓
Failure mode
↓
Failure effect
↓
Failure consequence
↓
Maintenance strategy
This is more powerful than simply preparing a generic PM checklist.
9. Start With Equipment Criticality
A steel plant may have thousands of components.
It is impossible to monitor every component with the same intensity.
Therefore, the first step should be:
Equipment Criticality Assessment
Classify equipment according to its consequence of failure.
Criticality factors
Consider:
Production impact
Safety impact
Environmental impact
Quality impact
Repair time
Spare availability
Failure frequency
Replacement cost
Redundancy
Effect on downstream equipment
A simple classification is:
| Class | Description | Maintenance Approach |
|---|---|---|
| A | Critical | PM + PdM + online monitoring where justified |
| B | Important | PM + periodic condition monitoring |
| C | Low criticality | Routine inspection / run-to-failure where appropriate |
10. Examples of Critical Steel Plant Equipment
Depending on plant configuration, critical assets may include:
Steel melting shop
Induction furnace
Furnace tilting system
Cooling-water system
Furnace transformer
Hydraulic system
Power supply
Charging equipment
Dust-extraction system
Continuous casting
Tundish system
Mould cooling system
Oscillation system
Withdrawal unit
Roll segments
Spray-water system
Hydraulic systems
Cutting system
Rolling mill
Main drive motors
Gearboxes
Pinion stands
Mill stands
Roll bearings
Cooling-water pumps
Hydraulic systems
Flying shear
Crop shear
Coil-handling equipment
Utilities
Compressors
Pumps
Cooling towers
Blowers
Transformers
Generators
Water-treatment systems
Material handling
EOT cranes
Conveyors
Hoists
Gearboxes
Wheels
Couplings
Brakes
11. Build an Equipment Master Register
Every critical machine should have a unique equipment ID.
The equipment master should contain:
Equipment number
Equipment name
Manufacturer
Model
Serial number
Installation date
Motor rating
Gearbox ratio
Bearing numbers
Lubricant specification
Normal operating temperature
Normal vibration level
Rated speed
Operating load
Maintenance history
Failure history
Spare-part information
Without reliable equipment identification, maintenance data becomes difficult to analyze.
12. Create Equipment Failure History
For every important breakdown, record:
Equipment
Date
Time
Failure component
Failure mode
Symptom
Root cause
Downtime
Repair duration
Spare used
Manpower
Corrective action
Permanent corrective action
This history becomes one of the most valuable sources of reliability information.
13. Failure Mode Analysis
Consider a gearbox.
Possible failure modes include:
Gear tooth damage
Bearing failure
Lubrication failure
Shaft failure
Seal failure
Misalignment
Overload
Contamination
Excessive temperature
Foundation looseness
Each failure mode requires a different detection method.
For example:
| Failure Mode | Possible Detection |
|---|---|
| Bearing damage | Vibration + temperature |
| Gear damage | Vibration + oil analysis |
| Lubrication failure | Oil analysis + temperature |
| Misalignment | Vibration |
| Overload | Current + process data |
| Seal failure | Visual inspection + oil leakage |
This is why a single condition-monitoring technology is rarely sufficient.
14. Vibration Analysis
Vibration analysis is one of the most useful predictive-maintenance techniques for rotating machinery.
It can identify conditions such as:
Unbalance
Misalignment
Mechanical looseness
Bearing defects
Gear defects
Resonance
Shaft problems
Coupling problems
Typical applications include:
Motors
Pumps
Fans
Blowers
Compressors
Gearboxes
Rolling-mill drives
Conveyors
15. Do Not Treat Vibration as Just One Number
A common mistake is to record only overall vibration.
A proper vibration program considers:
Overall vibration
Frequency spectrum
Waveform
Bearing frequencies
Harmonics
Sidebands
Trend
Operating speed
Load
For example, a change in spectral pattern may reveal a developing bearing defect even when overall vibration has not yet reached a severe level.
Therefore:
Trend + spectrum + engineering interpretation is much more useful than a single vibration number.
16. Vibration Trend Example
Consider a motor bearing:
| Month | Vibration |
|---|---|
| January | 1.8 |
| February | 1.9 |
| March | 2.0 |
| April | 2.3 |
| May | 2.8 |
| June | 3.5 |
| July | 4.4 |
The important observation is not merely the July value.
The important observation is the increasing trend.
This should trigger investigation.
Possible causes may include:
Bearing deterioration
Alignment change
Looseness
Unbalance
Lubrication problem
Foundation deterioration
The actual diagnosis must be based on measurements and equipment-specific limits.
17. Infrared Thermography
Thermography provides a non-contact method for identifying abnormal temperature patterns.
It is particularly useful for:
Electrical systems
MCCs
Switchgear
Transformers
Cable terminations
Busbars
Contactors
Breakers
Mechanical systems
Bearings
Motors
Gearboxes
Couplings
Brakes
Thermography is especially useful because many electrical faults manifest as localized heating before complete failure.
18. Electrical Connection Problems
Loose electrical connections can produce:
High resistance → heat generation → further deterioration → insulation damage → failure
Therefore, periodic thermal inspection of critical electrical equipment is valuable.
However, thermal images must be interpreted in context.
Compare:
Similar phases
Similar loads
Historical images
Ambient conditions
Equipment design
19. Lubrication Management
Lubrication should be treated as an engineering discipline.
A lubrication program should specify:
Lubricant
Grade
Quantity
Frequency
Application method
Storage conditions
Contamination controls
Temperature limits
Common lubrication failures include:
Under-lubrication
Over-lubrication
Wrong grease
Wrong oil viscosity
Mixing incompatible lubricants
Contamination
Water ingress
Poor storage
Incorrect application
20. Bearing Failures
Bearings are among the most common failure points in rotating equipment.
Common causes include:
1. Lubrication failure
Insufficient or degraded lubricant increases friction and temperature.
2. Contamination
Dust, water and scale can damage bearing surfaces.
3. Misalignment
Misalignment creates abnormal loading.
4. Overloading
Excessive radial or axial loads can shorten bearing life.
5. Incorrect installation
Improper mounting can damage bearing components.
6. Electrical damage
Electrical current passing through bearings can produce fluting and surface damage in certain motor applications.
21. Oil Analysis
Oil analysis is particularly valuable for:
Gearboxes
Hydraulic systems
Compressors
Large lubrication systems
Analysis can identify:
Wear metals
Contamination
Water
Viscosity changes
Oxidation
Additive depletion
Oil analysis becomes more powerful when results are trended rather than interpreted as isolated reports.
22. Hydraulic System Reliability
Hydraulic systems are widely used in steel plants.
Typical applications include:
Furnace tilting
Rolling mills
Shears
Lifting systems
Clamping systems
Manipulators
Material handling
Common hydraulic failures include:
Oil contamination
Pump wear
Valve sticking
Hose failure
Seal failure
Excessive temperature
Pressure loss
Air ingress
23. Hydraulic Oil Cleanliness
Hydraulic components can be sensitive to contamination.
Contamination sources include:
Dust
Metal particles
Water
Degraded seals
Poor filling practices
Good practices include:
Clean storage containers
Proper filtration
Filter monitoring
Closed filling systems
Regular oil analysis
Leak elimination
24. Cooling-Water System Reliability
Cooling water is a critical utility in many steel plants.
A cooling-water failure can rapidly create secondary equipment damage.
Monitor:
Flow
Pressure
Supply temperature
Return temperature
Pump vibration
Pump current
Leakage
Filter condition
Heat-exchanger condition
A critical cooling system should also be assessed for:
Pump redundancy
Emergency supply
Automatic changeover
Alarm systems
Low-flow protection
25. Motor Maintenance
Motors should be monitored for:
Current
Voltage
Temperature
Vibration
Bearing condition
Insulation
Load
Power factor
Starting behavior
Abnormal current may result from:
Mechanical overload
Supply imbalance
Bearing problems
Process overload
Rotor problems
Never assume that a tripping motor simply needs resetting.
Repeated trips should trigger an investigation.
26. Motor Current Signature Analysis
Motor current contains information about motor and mechanical condition.
Depending on application, analysis may help identify:
Rotor abnormalities
Load problems
Electrical imbalance
Mechanical abnormalities
This becomes particularly useful when combined with:
Vibration
Temperature
Process load
Electrical measurements
27. PLC and Instrumentation Reliability
Modern steel plants depend heavily on automation.
Failures can originate from:
Sensors
Proximity switches
Encoders
PLC I/O
Communication networks
Power supplies
Control cards
Signal cables
Instrument air
Software/configuration issues
Instrumentation maintenance should therefore be part of the reliability program.
28. Sensor Health Is Also Important
A predictive system is only as reliable as its measurements.
A faulty sensor can generate:
False alarms
Missed alarms
Incorrect trends
Wrong maintenance decisions
Therefore, sensor validation should include:
Calibration
Signal-quality checks
Comparison with redundant measurements
Inspection of wiring
Physical inspection
Plausibility checks
29. Preventive Maintenance Schedule
A practical maintenance schedule can use several levels.
Daily
Visual inspection
Leakage check
Abnormal noise
Temperature observation
Pressure check
Lubrication status
Safety-device status
Weekly
Detailed inspection
Lubrication checks
Fastener inspection
Belt/chain inspection
Electrical panel inspection
Monthly
Vibration route
Thermography
Motor inspection
Hydraulic inspection
Gearbox inspection
Quarterly
Detailed condition assessment
Oil sampling
Electrical testing
Alignment checks where required
Annual / Major Shutdown
Detailed mechanical inspection
Bearing inspection/replacement based on condition
Gearbox inspection
Motor overhaul as required
Electrical testing
Structural inspection
Calibration
Major alignment
The exact interval must be determined from equipment condition, manufacturer recommendations, duty cycle and plant experience.
30. Operator Maintenance
Operators are the first line of defense.
A trained operator can identify:
Unusual sound
Vibration
Leakage
Temperature increase
Smoke
Burning smell
Pressure change
Flow reduction
Abnormal motor sound
Hydraulic instability
Operator rounds should therefore become part of the maintenance system.
A simple principle is:
Operator detects → Maintenance diagnoses → Engineering solves → Management verifies
31. Autonomous Maintenance
Basic operator activities can include:
Cleaning
Inspection
Lubrication checks
Leak detection
Abnormality tagging
Tightness checks where permitted
Visual condition checks
The goal is not to turn operators into maintenance technicians.
The goal is to make abnormalities visible early.
32. Maintenance Work Orders
A maintenance system should convert detected abnormalities into controlled work orders.
A good work order contains:
Equipment
Problem description
Failure mode
Priority
Safety requirements
Spare parts
Tools
Estimated manpower
Planned duration
Job instructions
Inspection criteria
Completion confirmation
33. Maintenance Priority
A practical priority system might be:
Priority 1 — Emergency
Immediate safety or production risk.
Priority 2 — Critical
Failure likely within a short period; planned intervention required urgently.
Priority 3 — Routine
Condition requires correction but immediate failure is unlikely.
Priority 4 — Improvement
Reliability or efficiency improvement without immediate failure risk.
This prevents the maintenance team from treating every work order as an emergency.
34. Root Cause Analysis
When critical equipment fails, the question should not be:
"Which part failed?"
The question should be:
"Why did this part fail?"
For example:
Bearing failed
↓
Why?
High temperature
↓
Why?
Poor lubrication
↓
Why?
Incorrect grease quantity
↓
Why?
Lubrication procedure was not standardized
↓
Why?
No equipment-specific lubrication standard existed
The root cause is therefore not simply:
"Bearing failure."
The actual corrective action may be to improve the lubrication management system.
35. 5-Why Analysis
The 5-Why method is simple but powerful.
Example:
Problem
Rolling-mill gearbox stopped.
Why 1?
Gearbox temperature increased.
Why 2?
Lubrication was inadequate.
Why 3?
Oil level was low.
Why 4?
Oil leakage occurred through a damaged seal.
Why 5?
Seal deteriorated due to shaft misalignment.
The corrective action should therefore address alignment and seal reliability—not simply refill the gearbox.
36. Fishbone Analysis
A failure can also be classified into:
Man
Skill
Training
Procedure compliance
Machine
Wear
Design
Alignment
Overload
Method
Maintenance procedure
Inspection interval
Lubrication method
Material
Wrong lubricant
Poor-quality spare
Contaminated oil
Measurement
Faulty sensor
Incorrect calibration
Poor data
Environment
Heat
Dust
Water
Corrosion
This provides a structured approach to root-cause investigation.
37. Pareto Analysis of Breakdowns
Do not treat all failures equally.
Create a monthly Pareto chart showing:
Failure count
Downtime hours
Production loss
Maintenance cost
You may find that a small number of equipment groups are responsible for most losses.
Those assets should receive priority.
38. MTBF
Mean Time Between Failures (MTBF) is commonly used to measure reliability.
A simplified expression is:
MTBF = Operating Time / Number of Failures
Example:
If a pump operates 7,200 hours and experiences 6 failures:
MTBF = 7,200 / 6 = 1,200 hours
Increasing MTBF generally indicates improved reliability.
However, MTBF should always be interpreted together with equipment duty, operating conditions and failure definitions.
39. MTTR
Mean Time To Repair (MTTR) indicates how quickly equipment can be restored.
Simplified:
MTTR = Total Repair Time / Number of Repairs
Example:
If four repairs require a total of 20 hours:
MTTR = 20 / 4 = 5 hours
MTTR can be reduced through:
Proper spares
Better accessibility
Standardized procedures
Skilled technicians
Correct tools
Modular equipment
Better troubleshooting
Clear documentation
40. Availability
A simplified availability relationship is:
Availability ≈ MTBF / (MTBF + MTTR)
This demonstrates an important point.
Reliability and maintainability are both important.
A machine that rarely fails but requires 30 hours to repair can still create significant production problems.
41. Planned vs Unplanned Maintenance
A mature maintenance department should progressively increase the proportion of planned work.
The objective is to reduce:
Emergency → Unplanned → Reactive
and increase:
Planned → Condition-based → Predictive → Reliability improvement
This does not mean eliminating all corrective maintenance.
It means making maintenance more predictable.
42. Critical Spare Parts Strategy
Critical equipment requires critical spares.
Examples:
Motors
Gearboxes
Bearings
Pumps
Hydraulic valves
PLC modules
Sensors
Encoders
Contactors
Breakers
Couplings
Seals
Spare classification should consider:
Criticality + Lead Time + Failure Probability + Cost
A low-cost item with a six-month lead time can be more critical than an expensive item available locally within hours.
43. Preservation of Spare Parts
A spare is not useful if it has deteriorated while sitting in stores.
Depending on equipment, storage controls may be needed for:
Motors
Bearings
Electronic cards
Hydraulic components
Rubber seals
Batteries
Gearboxes
Store critical components according to manufacturer recommendations.
44. Shutdown Planning
Planned shutdowns are valuable opportunities for major maintenance.
A good shutdown should begin with:
Scope freeze
Clearly define what will be done.
Material readiness
Confirm all critical spares.
Manpower
Identify internal and contractor resources.
Tools
Ensure specialized tools are available.
Safety
Prepare isolation and permit requirements.
Work sequence
Identify critical-path activities.
Inspection
Define acceptance criteria.
Start-up
Prepare commissioning and monitoring procedures.
45. Do Not Turn Every Shutdown Into a Replacement Campaign
A common mistake is replacing components simply because the plant is stopped.
Before replacement, ask:
What is the failure history?
What is the measured condition?
What is the remaining useful life?
What is the consequence of failure?
Is replacement technically justified?
Condition-based decisions can prevent unnecessary expenditure.
46. Digital Maintenance and CMMS
A CMMS can integrate:
Equipment register
PM schedules
Work orders
Breakdown history
Spare parts
Maintenance manpower
Inspection results
Failure analysis
However:
Software does not create reliability by itself.
Poor data entered into a sophisticated CMMS still produces poor decisions.
The quality of equipment hierarchy, failure codes, inspection data and maintenance discipline is critical.
47. From CMMS to Predictive Maintenance
The next step is connecting condition data with maintenance decisions.
For example:
Vibration sensor
↓
Condition-monitoring platform
↓
Abnormal trend
↓
Engineering review
↓
Work order
↓
Planned shutdown
↓
Component replacement
↓
Failure avoided
This closes the loop between measurement and action.
48. Artificial Intelligence in Steel Plant Maintenance
AI and machine learning can support predictive maintenance by analyzing large quantities of sensor and process data.
Potential applications include:
Anomaly detection
Failure classification
Remaining useful life estimation
Bearing-wear prediction
Energy anomaly detection
Process-equipment correlation
Predictive alarms
Research on steel components has also explored digital twins and AI-based remaining-useful-life prediction.
Research specifically examining AI-based predictive maintenance in the steel industry shows growing interest in applications across areas such as blast furnaces and hot rolling.
But AI should not replace engineering judgment.
A model can identify an abnormal pattern.
An engineer must determine:
What does the abnormality mean?
What failure mechanism is likely?
What action should be taken?
49. The Importance of Data Quality
Predictive maintenance depends heavily on good data.
Important data sources include:
Vibration
Temperature
Pressure
Flow
Motor current
Speed
Load
Oil condition
Maintenance history
Production conditions
Data should be:
Accurate
Time-stamped
Properly identified
Consistent
Contextualized
For example, a vibration reading without knowing machine speed and load may be difficult to interpret.
50. Human Expertise Remains Essential
A successful predictive-maintenance system is not:
Sensors + AI = Reliability
It is:
Sensors + Data + Engineering Knowledge + Maintenance Process + Human Decision-Making = Reliability
A recent industrial example also illustrates this point: successful sensor deployment required collaboration between reliability personnel and technology providers to interpret large volumes of vibration data and integrate other condition-monitoring techniques.
51. Reliability Dashboard
A plant reliability dashboard should ideally display:
Production
Production availability
Downtime
Lost production
Reliability
MTBF
Repeat failures
Critical equipment health
Maintenance
MTTR
PM compliance
Planned maintenance %
Backlog
Condition Monitoring
Critical alarms
Vibration trends
Temperature alarms
Oil-analysis abnormalities
Spare Parts
Critical stock
Stock-outs
Lead-time risks
52. Equipment Health Score
For critical assets, a plant can create a simple health index.
For example:
| Parameter | Weight |
|---|---|
| Vibration | 25% |
| Temperature | 15% |
| Lubrication/Oil | 20% |
| Electrical condition | 15% |
| Operating load | 10% |
| Maintenance history | 15% |
The exact weights must be engineered for the specific equipment.
The objective is to provide a common decision-support framework.
53. Equipment Health Categories
A practical dashboard can classify equipment as:
Healthy
Normal condition.
Watch
Abnormal trend requiring investigation.
Action Required
Planned intervention required.
Critical
Immediate engineering/maintenance action required.
The colors are communication aids, not substitutes for engineering limits.
54. Equipment-Wise Predictive Maintenance Matrix
| Equipment | Main Failure Modes | Recommended Techniques |
|---|---|---|
| Motor | Bearing, insulation, overload | Vibration, thermography, electrical tests |
| Pump | Bearing, seal, cavitation | Vibration, pressure, temperature |
| Gearbox | Gear wear, bearing, lubrication | Vibration, oil analysis, temperature |
| Fan | Unbalance, bearing | Vibration, temperature |
| Compressor | Bearing, valve, lubrication | Vibration, oil analysis, temperature |
| Conveyor | Bearing, belt, gearbox | Vibration, visual, thermography |
| Hydraulic system | Pump, valve, contamination | Oil analysis, pressure, temperature |
| Transformer | Heating, insulation | Thermography, oil tests, electrical tests |
| MCC | Loose connections, overload | Thermography, electrical inspection |
| Crane | Brake, gearbox, wheel, motor | Vibration, visual, electrical tests |
| Rolling mill drive | Gear, bearing, motor | Vibration, oil analysis, electrical monitoring |
55. Example: Preventing a Rolling-Mill Gearbox Failure
Consider a gearbox driving a rolling stand.
Initial condition
Normal vibration.
Month 1
Slight increase in vibration.
Month 2
Gear-mesh frequency begins changing.
Month 3
Oil analysis detects increased wear particles.
Engineering assessment
Possible gear/bearing degradation.
Action
Maintenance is scheduled during the next planned shutdown.
Inspection
A developing gear-tooth defect is discovered.
Result
The component is replaced before catastrophic gearbox failure.
The key point is that:
Vibration + oil analysis + trend + engineering diagnosis
created enough warning to plan the intervention.
This is the essence of predictive maintenance.
56. Example: Preventing Motor Failure
Suppose a critical pump motor shows:
Increasing bearing temperature
Increasing vibration
Slight current increase
Instead of replacing the motor immediately, the team investigates.
Possible causes:
Pump misalignment
Bearing degradation
Coupling problem
Mechanical overload
If alignment is found to be incorrect and corrected early, the motor may continue operating safely.
The objective is not merely to predict the failure.
The objective is to prevent the failure.
57. Example: Preventing Electrical Breakdown
An MCC feeder shows a significantly higher temperature at one termination compared with similar phases.
Investigation reveals:
Loose termination
Increased contact resistance
Corrective action:
Isolate equipment safely
Inspect connection
Correct termination
Verify thermal condition after return to service
A relatively small intervention can prevent:
Cable damage
Insulation failure
Arc-related damage
Production interruption
58. Common Maintenance Mistakes
Mistake 1: "Run it until it breaks."
Acceptable only for selected low-consequence equipment.
Mistake 2: Replacing parts without identifying the cause.
This creates repeat failures.
Mistake 3: Collecting condition data without trending it.
A single reading has limited value.
Mistake 4: Installing sensors without a maintenance workflow.
An alarm is useless if nobody acts on it.
Mistake 5: Ignoring lubrication.
Many mechanical failures begin with lubrication problems.
Mistake 6: Poor spare management.
A small unavailable component can stop a major production line.
Mistake 7: Treating every machine equally.
Maintenance resources should follow risk.
Mistake 8: Ignoring operator knowledge.
Operators often detect abnormalities before instruments do.
59. 20 Practical Actions to Reduce Steel Plant Breakdowns
Create an equipment hierarchy.
Identify critical assets.
Develop failure-mode lists.
Establish PM standards.
Develop operator inspection routes.
Introduce vibration monitoring.
Introduce thermography.
Establish lubrication standards.
Implement oil analysis for critical systems.
Monitor critical motors.
Monitor hydraulic systems.
Improve cooling-system reliability.
Maintain critical instrumentation.
Record every breakdown.
Conduct RCA for major failures.
Analyze repeat failures.
Maintain critical spares.
Improve shutdown planning.
Track MTBF and MTTR.
Continuously improve maintenance standards.
60. A 90-Day Reliability Improvement Plan
A plant does not need to install an expensive Industry 4.0 system on day one.
A practical implementation can begin with a 90-day program.
Days 1–30: Assessment
Identify:
Top 20 critical assets
Top 20 failure modes
Major downtime causes
Repeat failures
Critical spare shortages
PM gaps
Lubrication problems
Existing condition-monitoring capability
Days 31–60: Control
Implement:
Critical-equipment PM
Operator inspection
Lubrication standards
Breakdown coding
RCA for critical failures
Spare-part review
Basic vibration routes
Electrical thermography
Days 61–90: Predict
Start:
Equipment trending
Condition-based maintenance
Critical asset dashboards
Oil analysis
Online sensors where justified
CMMS integration
Reliability KPI reviews
61. One-Year Reliability Roadmap
Quarter 1
Stabilize
Equipment hierarchy
PM standards
Criticality
Basic inspection
Breakdown recording
Quarter 2
Measure
Vibration
Thermography
Oil analysis
Electrical monitoring
KPI dashboards
Quarter 3
Predict
Condition-based maintenance
Automated alarms
Trend analysis
Critical asset monitoring
Quarter 4
Optimize
RCA improvement
AI/predictive analytics where justified
Reliability-centered maintenance
Spare optimization
Maintenance strategy review
62. The Reliability Improvement Cycle
A mature plant should continuously repeat:
Identify
↓
Measure
↓
Analyze
↓
Act
↓
Verify
↓
Standardize
↓
Improve
This prevents maintenance from becoming a repetitive cycle of repair without learning.
63. Maintenance Culture
Technology alone cannot eliminate breakdowns.
A strong reliability culture requires:
Management commitment
Skilled maintenance teams
Trained operators
Accurate data
Standard procedures
Cross-functional cooperation
Strong safety culture
Accountability
Continuous improvement
The maintenance department should not be viewed simply as the department that repairs machines.
It should be viewed as:
The department responsible for preserving production capability.
64. Operations and Maintenance Must Work Together
A common organizational problem is:
Operations: "Maintenance is causing downtime."
Maintenance: "Operations is damaging equipment."
This approach creates conflict.
A better model is:
Operations + Maintenance + Engineering = Equipment Reliability Team
Operations provides:
Operating conditions
Process changes
Abnormal behavior
Load information
Maintenance provides:
Condition data
Failure history
Inspection results
Repair information
Engineering provides:
Root-cause analysis
Design improvements
Reliability solutions
Together, they can eliminate recurring failures.
65. Safety Must Come Before Reliability
No maintenance strategy should compromise safety.
Before inspection or maintenance:
Follow plant isolation procedures.
Apply lockout/tagout requirements where applicable.
Verify zero-energy state.
Control stored energy.
Follow electrical safety procedures.
Follow hot-work requirements.
Follow confined-space procedures.
Use appropriate PPE.
Follow plant-specific safety standards.
A machine that is available but unsafe is not a reliable asset.
66. Maintenance and Energy Efficiency
Reliability and energy efficiency are connected.
Poor mechanical condition can increase:
Friction
Motor load
Hydraulic losses
Compressed-air consumption
Pumping energy
Examples:
Misalignment → vibration → friction → higher energy consumption
Dirty filter → pressure drop → higher pump/compressor load
Poor lubrication → friction → heat → energy loss
Therefore, predictive maintenance can contribute not only to reliability but also to energy management.
67. Maintenance and Product Quality
Equipment condition can directly influence steel quality.
Examples:
Rolling-mill vibration can influence dimensional stability.
Cooling-system problems can affect process conditions.
Sensor failures can affect control accuracy.
Hydraulic instability can affect equipment movement.
Furnace equipment problems can affect process control.
Therefore:
Equipment reliability → Process stability → Product quality
68. Maintenance and Production Planning
Maintenance should be integrated with production planning.
Instead of waiting for equipment to fail, maintenance can identify:
"This gearbox requires intervention within the next 100 operating hours."
Production can then determine:
Suitable shutdown window
Production sequence
Spare availability
Manpower
Contractor requirements
This converts maintenance from an emergency activity into a planned business process.
69. The Most Important Principle
The most important principle in reliability engineering is:
Do not simply repair failures. Eliminate failure mechanisms.
If the same pump bearing fails five times in one year, the objective should not be:
"Replace the bearing faster."
The objective should be:
"Determine why the bearing keeps failing and eliminate the cause."
That could involve:
Alignment
Lubrication
Load
Installation
Contamination
Pump operating point
Foundation
Coupling
Design modification
70. Final Reliability Framework
A highly effective steel plant reliability system can be represented as:
Equipment Criticality
↓
Failure Mode Analysis
↓
Preventive Maintenance
↓
Condition Monitoring
↓
Predictive Maintenance
↓
Planned Intervention
↓
Root Cause Analysis
↓
Reliability Improvement
↓
Performance Measurement
↓
Continuous Improvement
This is the foundation of a modern maintenance organization.
71. Final Conclusion
Reducing breakdowns in a steel plant is not achieved by purchasing more spare parts or hiring more maintenance personnel.
It requires a systematic approach to equipment reliability.
The most successful strategy combines:
Preventive Maintenance
Predictive Maintenance
Condition Monitoring
Reliability-Centered Maintenance
Root Cause Analysis
Skilled People
Accurate Data
Good Spare Management
Strong Safety Practices
Continuous Improvement
The ultimate objective is not zero maintenance.
It is not zero corrective work.
It is not simply maximum equipment utilization.
The real objective is:
Maximum safe production with minimum unplanned downtime.
A modern steel plant should continuously move from:
Reactive → Preventive → Condition-Based → Predictive → Reliability-Centered
The future will increasingly combine sensor data, industrial analytics, digital twins and AI with experienced engineers and technicians. Research already demonstrates applications of data-driven predictive maintenance in steel production, while newer work explores digital-twin and AI approaches for remaining-useful-life prediction.
But technology is only one part of the solution.
The foundation remains:
Good engineering + good maintenance practices + good data + skilled people + disciplined execution.
When these elements work together, equipment becomes more reliable, production becomes more stable, maintenance becomes more predictable and the plant becomes safer and more competitive.
MetaTechX Engineering Knowledge Series
At MetaTechX, our objective is to make practical industrial knowledge accessible to engineers, technicians, operators and professionals working in the manufacturing and steel industries.
Explore more technical subjects covering:
Steel Making | Induction Furnace | Continuous Casting | Rolling Mill | ERW Tube Manufacturing | Mechanical Maintenance | Electrical Maintenance | PLC & Automation | Industrial Safety | Reliability Engineering | Steel Plant Operations
Assess. Certify. Get Recognized. Get Preferred.
Technical knowledge becomes more valuable when it can be demonstrated.
Professionals can use MetaTechX GetCertified to assess and demonstrate their technical knowledge and skills.
Key message for the article
The objective of modern maintenance is not to repair failures faster. It is to identify degradation earlier, understand why failures occur, and intervene before the failure becomes a production breakdown.
Comments 0
Be the first to share your thoughts.
Leave a comment
Your comment will appear after a quick moderation check.